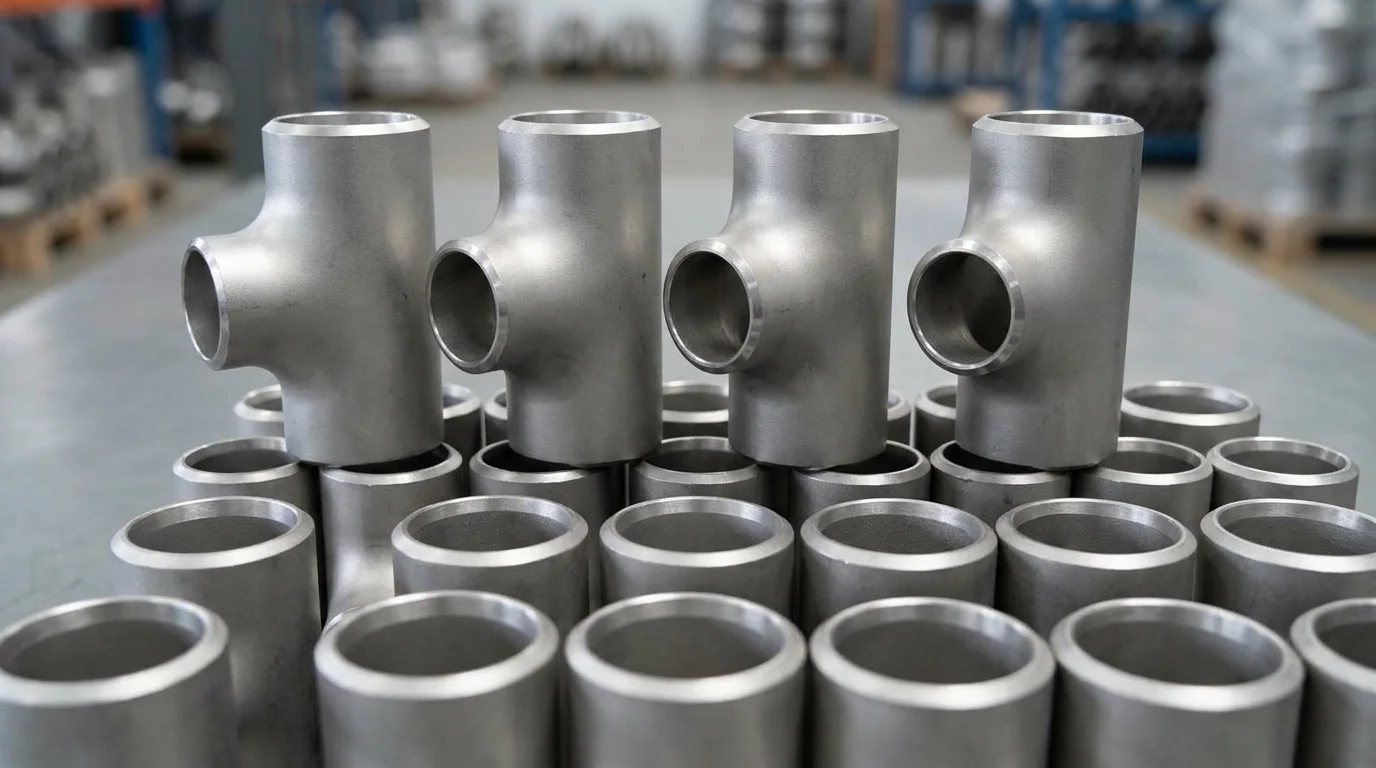
Threaded vs Butt Weld Fittings: Which to Choose in UAE 

Use threaded fittings for low-pressure, non-critical, smaller-scale lines (NPS 2 and below) that need frequent maintenance, such as water distribution or air lines. Use butt weld fittings for critical, high-pressure, high-temperature service in oil and gas, petrochemical plants, refineries, and power generation.

Choosing between threaded vs butt weld fittings looks like a routine procurement decision. It is not. The wrong joint type causes leaks, rework, and failed inspections, especially in UAE plants where heat, humidity, and saline air punish weak connections.

This guide gives engineers and procurement leads a practical framework for matching each joint to its service, using ASME standards and field conditions common across the Emirates.

What Separates Threaded vs Butt Weld Fittings?

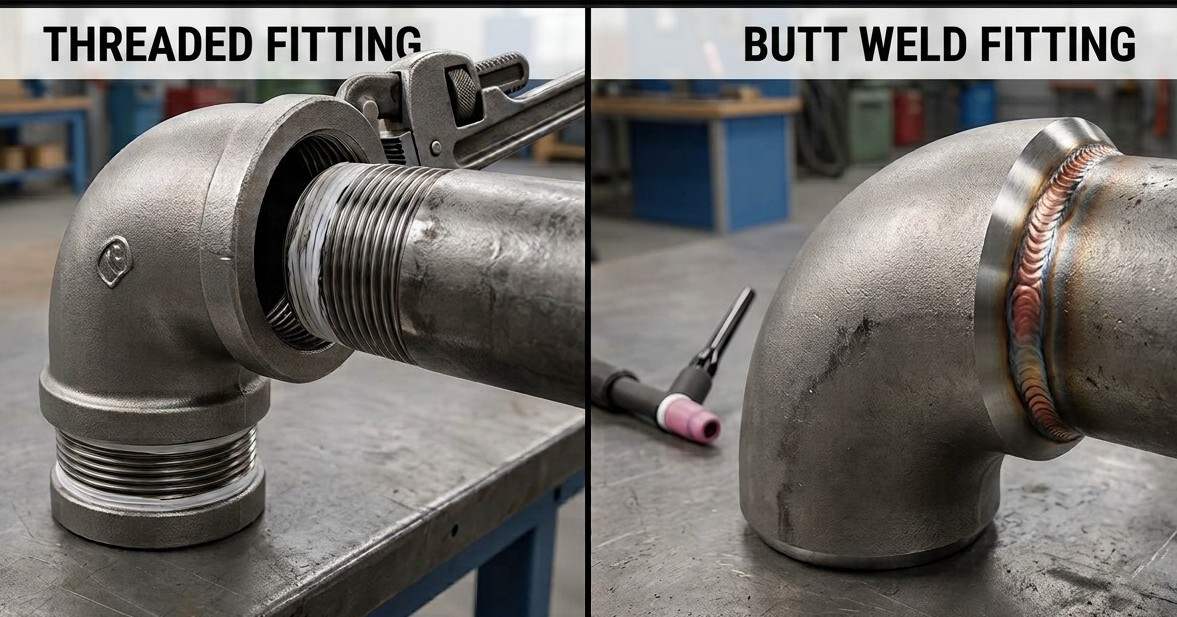
Threaded fittings join pipe through tapered screw threads, while butt weld fittings join pipe through a full-penetration weld at beveled ends. The threaded joints install quickly without welding labor, and butt weld joints create a continuous metal path for critical service.

Threaded fittings follow ASME B16.11 and use NPT threads defined in ASME B1.20.1. Butt weld fittings follow ASME B16.9 and are installed under ASME B31.3 process piping rules.

When Should You Use Threaded Fittings?

Threaded fittings are best for low-pressure, non-critical, and smaller-scale systems requiring frequent maintenance or modifications, such as water distribution or air lines. They typically serve NPS 2 and below, and suit areas where hot work is restricted or welding is impractical.

Three limits matter in practice:

  • Thread sealant degrades under thermal cycling and vibration.
  • Cut threads thin the pipe wall, so Schedule 80 or heavier is standard practice.
  • Thread roots trap moisture, which accelerates crevice corrosion in coastal environments.

Avoid threaded joints on cyclic, vibrating, or toxic lines. Every thread is a potential leak path and a stress concentration point.

Unsure which joint your piping class allows? Request a fittings specification review before you finalize the material take-off.

Why Are Butt Weld Fittings Essential for Critical Service?

Butt weld fittings are essential for critical, high-pressure, and high-temperature industries like oil and gas, petrochemical plants, refineries, and power generation. The full-penetration weld removes the leak path and allows radiographic or ultrasonic examination of every joint.

Demand for butt weld fittings in UAE projects follows the region’s industrial base. Process headers in upstream facilities, refineries, and desalination plants rely on welded joints because operators cannot tolerate leaks in hydrocarbon or steam service.

Butt weld work demands qualified welders, approved welding procedure specifications, and post-weld inspection. Those requirements add schedule and labor cost. Over a 25-year asset life, however, fewer leak events usually outweigh the upfront expense.

How Do Threaded vs Butt Weld Fittings Compare on Cost and Risk?

Threaded fittings cost less to install and allow quick disassembly, but they carry lower practical pressure ratings and higher leak risk. Butt weld fittings cost more to install and cannot be dismantled without cutting, yet they deliver the strongest joint and the lowest lifecycle leak rate.

  • Pressure: Threaded fittings reach Class 6000 under B16.11, but field limits sit lower. Butt weld fittings match the pipe schedule rating.
  • Inspection: Threaded joints cannot be radiographed. Butt welds accept RT and UT.
  • Flow: Butt welds keep a smooth bore, while threads create turbulence and erosion points.
  • Maintenance: Threaded joints unscrew. Welded joints require cutting and rewelding.
  • Upfront cost: Threaded joints win on small sizes.

What Framework Should You Use to Select the Right Fitting?

Score four factors before selecting: fluid hazard, pressure and temperature, line size, and maintenance access. If fluid hazard or pressure is high, choose butt weld. If the line is small, low-risk, and needs frequent removal, choose threaded.

Run this checklist for each line class:

  1. Classify the fluid under ASME B31.3 as Normal, Category D, or Category M.
  2. Compare design pressure and temperature against the piping class rating.
  3. Restrict threaded joints to NPS 2 and below.
  4. Confirm material and corrosion allowance for saline or high-humidity exposure.
  5. Verify welder qualification and inspection capacity before committing to welded joints.
  6. Record the decision in the piping class so contractors cannot substitute joints on site.

Audit field substitutions during construction. Contractors often swap joint types to save time, and those changes rarely pass back through design review.

Conclusion

The threaded vs butt weld fittings decision comes down to hazard, pressure, size, and access. Use threaded joints sparingly on small, low-risk lines and default to butt weld for anything critical. K Hashim LLC helps UAE project teams match fittings to piping classes and avoid costly specification errors. Schedule a consultation with our team before your next material take-off.

Choose the right fittings the first time

Tell us your pipe size, material grade, pressure class, and service conditions. Our team will recommend suitable threaded or butt weld fittings with the documents your inspector expects. You get clear guidance and a prompt quote for your project.

Request a Fittings Quote

Frequently Asked Questions

Can threaded fittings handle high-pressure service?

Threaded fittings can carry high pressure on paper, since ASME B16.11 covers Class 6000 ratings for small sizes. In practice, vibration, thermal cycling, and thread leakage make them unsuitable for most high-pressure hydrocarbon lines and any toxic or flammable service.

Which joint resists UAE coastal corrosion better?

Butt weld joints resist coastal corrosion better because they have no thread roots to trap moisture and salt. Material choice still decides final performance in chloride-rich service, so specify 316L, duplex stainless, or coated carbon steel to match the environment.

Which standards govern these fittings?

ASME B16.11 governs forged threaded and socket weld fittings, and ASME B16.9 governs factory-made wrought butt weld fittings. ASME B31.3 sets the process piping design, welding, and inspection rules that determine which joint types your project may use.

Explore More Expert Insights

Explore our expert insights to learn more about buttweld fittings, their types, standards and practical applications.

7 Common Mistakes People Make When Buying Butt Welded Fittings 

  • Most butt weld fitting problems start at purchasing, not on site.
  • Supplier quality, material choice and dimensional standards decide how smoothly welding goes.
  • Test certificates, heat numbers and traceability protect you during inspection.
  • Pressure rating, pipe schedule and fitting type must match the real layout and operating conditions.
  • Comparing total project cost beats chasing the lowest quotation.

Buying the right butt welded fittings can make a big difference to the performance of a piping system. However, small mistakes during purchasing can lead to poor fit-up, welding problems and extra costs later.

In this guide, we’ll cover 7 common mistakes people make when buying butt welded fittings and explain what you should check before placing an order. This will help you choose the right fittings and avoid problems during installation and operation.

What Buyers Should Know Before Selecting Butt Weld Fittings

Butt weld fittings are installed as part of a piping system and must handle the same pressure and temperature conditions as the connected pipe. They are used to change direction, split flow, reduce pipe size or close the end of a line. Choosing the wrong fitting can lead to poor fit-up, welding issues and problems during operation.

Many piping problems start with small details that are overlooked during purchasing. Checking the material, dimensions, pressure rating and required standards before placing an order can help prevent these issues. Understanding the 7 common mistakes people make when buying butt welded fittings makes it easier to ask the right questions and choose fittings that suit the application.

If you are new to this product range, our ultimate guide to buttweld fittings explains sizes, materials and common uses in plain language.

The Seven Buying Mistakes at a Glance

Here is a quick view of what goes wrong and how to prevent it. Each numbered point is explained in the sections that follow, and the 7 mistakes people make when buying butt welded fittings are easier to avoid once they are laid out side by side.

No Mistake What Goes Wrong How to Prevent It
1 Treating all suppliers alike Uneven quality between batches Review production and inspection records
2 Buying on material cost alone Corrosion and early replacement Match grade to the operating environment
3 Ignoring dimensional standards Poor fit up and slow welding Confirm ASME B16.9 compliance
4 Skipping inspection documents No proof of origin or grade Ask for test certificates before ordering
5 Overlooking pressure rating Stress cracks over time Check schedule and design pressure
6 Choosing the wrong fitting type Flow loss and extra stress Match type and radius to the layout
7 Chasing the lowest price Rework and delays Compare total project cost

Mistakes One to Three That Start at Supplier Selection

The first three mistakes happen before an order is placed, while suppliers, materials and standards are still being compared.

1. Treating Every Supplier as the Same

On a catalogue page an elbow looks like an elbow. On site the difference shows in machining quality, wall thickness consistency and bevel finish. Two suppliers can quote the same size and grade and still deliver very different results.

Look at how the fittings are made and tested, not just the price. A reliable buttweld fittings supplier will explain the production route, share inspection procedures and point to previous project supply.

2. Choosing Material Based on Budget Alone

Material choice should follow the operating environment. A coastal or offshore line faces very different corrosion than an inland utility line. Stainless steel butt weld fittings cost more upfront, yet they often reduce maintenance in chemical, marine and food processing service. Carbon steel remains a sound choice for general oil, gas and water lines where corrosion is under control.

The fitting grade must also suit the pipe and the fluid. A mismatch usually shows up later as pitting, scaling or failure at the weld.

3. Ignoring Dimensional Standards and Tolerances

Many buyers assume every supplier follows the same dimensions. That assumption is expensive. Outer diameter, wall thickness and bevel angle must line up with the pipe for a clean root pass.

Fittings made to ASME B16.9 follow recognised dimensions, which keeps fit up consistent from one batch to the next. Ask for confirmation of dimensional tolerances in writing, especially on large orders delivered in stages.

Good dimensions also make the welder’s job easier once the order arrives, and it helps to review the common installation mistakes before welding begins.

Mistakes Four to Seven That Surface During Installation and Operation

The next four mistakes often stay hidden at the purchasing stage and only show up during inspection, welding and daily operation.

4. Skipping Inspection Documents and Traceability

Material test certificates, heat numbers and traceability records may feel like paperwork. They become valuable the moment an inspector asks where a fitting came from. Request these documents before the order is confirmed, not after delivery. If a supplier hesitates, treat that as useful information.

5. Overlooking Pressure Rating and Pipe Schedule

Every fitting has a working limit that depends on wall thickness and material grade. Check the pressure class against your design pressure and confirm the pipe schedule, since an unspecified schedule often defaults to standard wall.

Underrated fittings rarely fail on day one. They develop stress cracks under cyclic pressure over months. For high pressure and critical lines, many engineers prefer seamless butt weld fittings because of their uniform structure.

6. Picking the Wrong Fitting Type for the Layout

Elbows, tees, reducers and caps each do a specific job. Long radius elbows reduce turbulence and pressure drop in most layouts, while short radius versions suit tight spaces. Concentric reducers suit vertical lines, and eccentric reducers help avoid trapped air or liquid in horizontal runs. Choosing by habit instead of by layout creates flow restrictions and extra stress.

To match each fitting to its job, read about the types of buttweld fittings and where each one is used.

7. Chasing the Lowest Price

A low quotation looks like a win until labour hours start climbing. Extra fit up time, rework and delayed testing quickly cancel any saving. Experienced project managers compare the full cost, including lead time, documentation and after sales support. This is why the 7 mistakes people make when buying butt welded fittings so often trace back to price pressure at the quotation stage.

A Practical Checklist Before You Place an Order

Run through these points with your supplier before confirming any purchase.

  • Confirm the material grade against the pipe specification and the fluid
  • Request material test certificates and heat numbers
  • Verify ASME B16.9 compliance and agree tolerances
  • Check pressure class and pipe schedule against design data
  • Match fitting type and radius to the layout
  • Compare lead time and support along with price

Final Thoughts

Most piping problems start at procurement, long before the first weld. Supplier checks, material choice, standards, documents, pressure ratings, fitting type and total cost all deserve attention, and the 7 mistakes people make when buying butt welded fittings become simple to avoid once you know where to look.

If you are comparing options for your piping needs, K Hashim LLC is a good place to look through available products and get a clearer picture of what suits your application.

Buy the right buttweld fittings the first time

Tell us your pipe size, material grade and pressure requirements, and our team will recommend suitable fittings with the documents your inspector expects. You get clear guidance and a prompt quote for your project.

FAQs

What are butt weld fittings used for?

They connect pipes by welding, allowing a line to change direction, branch, reduce in size or end with a cap. Their smooth internal profile supports steady flow in oil, gas, marine and process piping.

Should I choose seamless or welded butt weld fittings?

Seamless fittings suit high pressure and critical service because of their uniform structure. Welded fittings work well for general lines and larger sizes where pressure demands are moderate. The right choice depends on your design pressure and project specification.

Which standard applies to butt weld fittings?

ASME B16.9 is the standard most buyers rely on for dimensions and tolerances of factory made butt weld fittings. Always confirm the exact standard and material grade in your purchase order.

Explore More Expert Insights

Explore our expert insights to learn more about buttweld fittings, their types, standards and practical applications.